Fine chemical industry is a key sector for manufacturing high value-added chemicals, covering sub-segments such as pesticide intermediates, pharmaceutical API, dyes & pigments, electronic chemicals and daily chemicals. Its production processes are dominated by batch operation. Pump equipment is relied on for medium transfer and metering in processes including reactor feeding, solvent recovery, product purification and waste liquid treatment.
Fine Chemicals
Introduction to Related Products
-
Oleochemical Service
Oleochemical industry is a process industry that uses natural oils and fats (vegetable oils, animal fats) as raw materials to produce fatty acids, fatty alcohols, glycerin, soap, lubricant additives and other products through refining, modification, cracking and other processes. Its production process covers crude oil pretreatment, degumming and deacidification, decolorization and deodorization, followed by fatty acid distillation and separation, fatty alcohol hydrogenation, saponification reaction, and finally finished product filling, storage and transportation. Pump equipment is required for medium transfer and process support in every stage.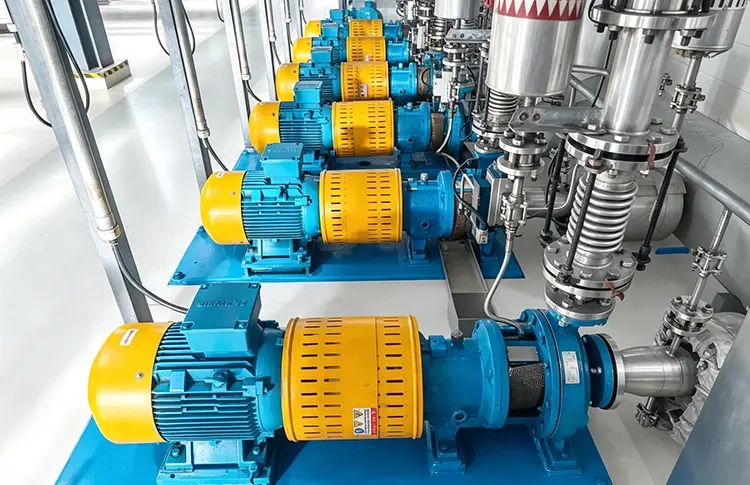
-
Agrochemical Service
Agrochemical industry is one of the most demanding sub-sectors within the fine chemical industry. Pesticide production mainly adopts batch operation, covering multiple stages including technical material synthesis, intermediate preparation and formulation processing. Pumping equipment is required to perform material transfer, metered dosing and solvent recovery under service conditions of heavy corrosion, high solid content, toxic & hazardous, flammable and explosive media.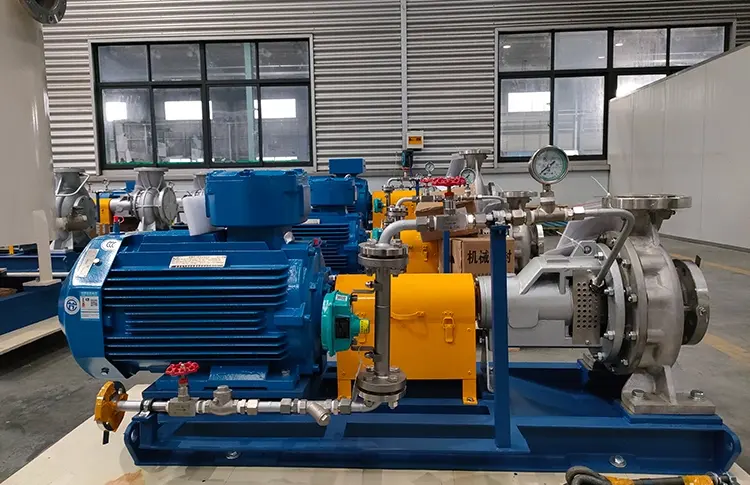
-
Daily Chemical Service
The daily chemical industry involves the manufacturing of toothpaste, shampoo, body wash, skin cream, laundry detergent, dishwashing liquid and other products. It is one of the most mature and widely adopted application fields for cam rotor pumps. Cam rotor pumps play an important role in upstream and downstream segments of the daily chemical industry. They are used for transferring materials including LAS, AES, AOS, MES, K12, glycerin, sorbitol, skin cream, cosmetics, toothpaste, facial cleanser, lotion, shampoo, body wash, liquid soap, dishwashing liquid and detergent slurry.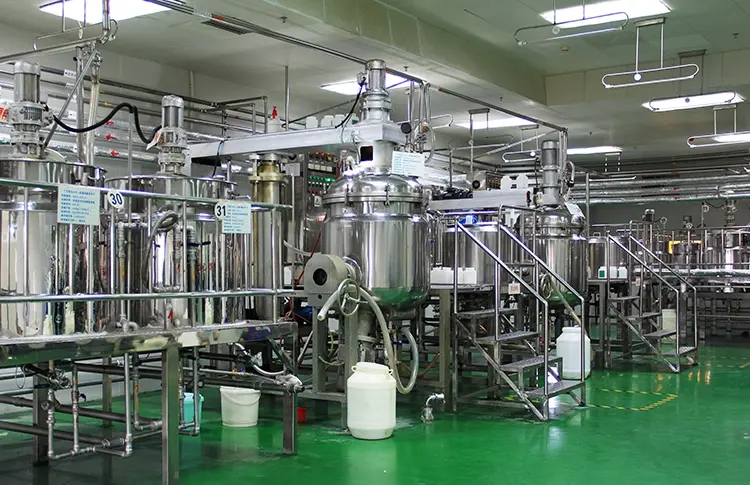
Relevant Cases
Anhui Guotai Pump has always put the interests of customers in the first place, customers satisfaction as the fundamental development of the enterprise. To provide customers with the whole product life cycle services,and fully meet the differentiated needs of customers
-
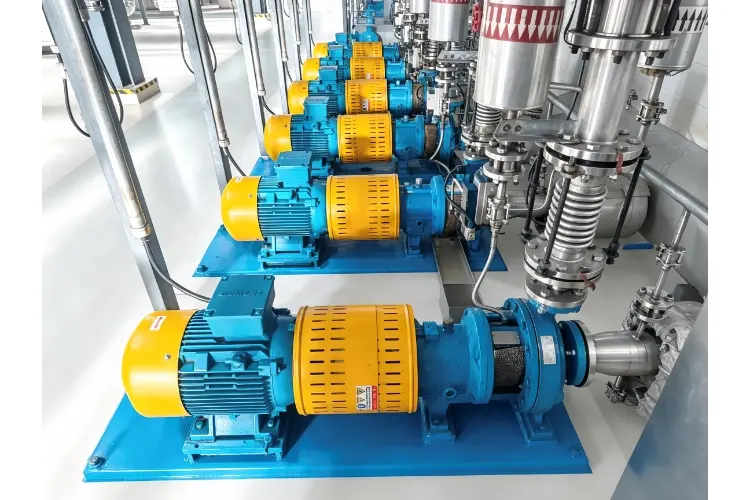
NXH Series Chemical Centrifugal Pumps for a Large-Scale Edible Oil Refinery Upgrade
Operating Conditions: The refinery processes 560 tons of crude oil per day. The bleaching section is equipped with three bleaching pumps, operating in a 2-running + 1-standby configuration. Each pump is driven by a 30 kW motor. The origi...
Learn More -
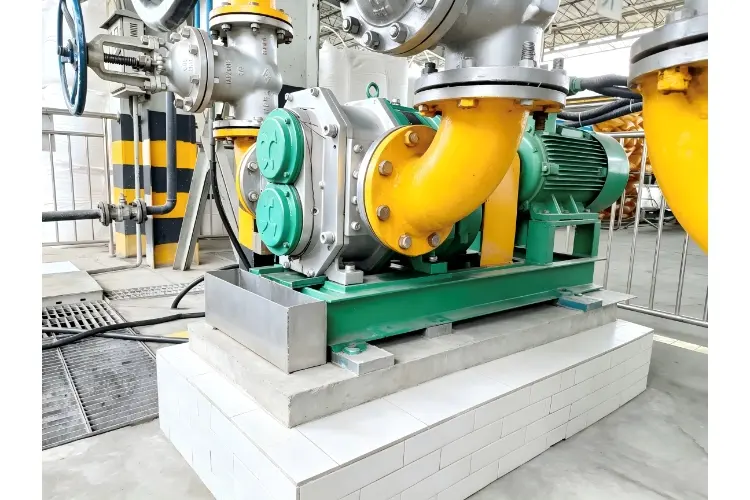
Rotor Pump Replaces Centrifugal Pump in a Fatty Acid Production Plant
A fatty acid production plant previously used centrifugal pumps to transfer fatty acid. During actual operation, three major issues became apparent: 1. Low Transfer Efficiency Fatty acid has a certain level of viscosity, causing the cent...
Learn More -
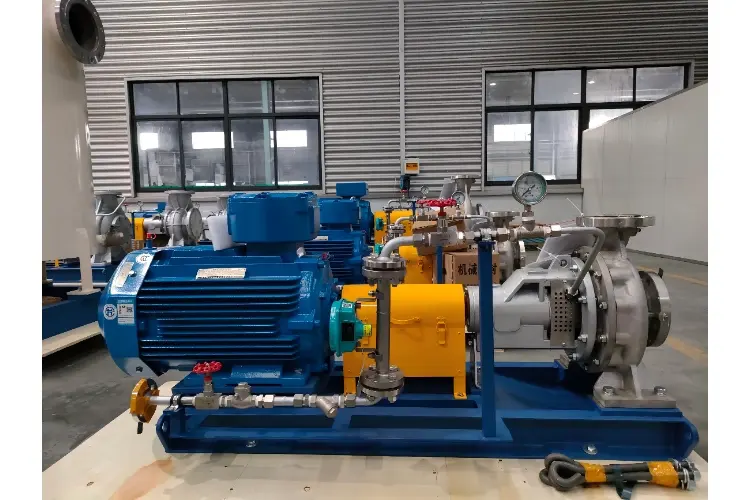
Pesticide Formulation Blending and Transfer Project
Equipment Selected:The project utilizes chemical process pumps as part of the complete pumping system. Operating Conditions:The project is a pesticide intermediate production facility with an annual capacity of 10,000 tons of fluroxy...
Learn More
Welcomes Your Consultation
Anhui Guotai Pump Technology Co., Ltd. is a comprehensive pump enterprise specializing in the research, development, design, manufacturing, sales, and technical service of Centrifugal pump、 Rotor pump, complete energy-saving pumping systems, and pump control equipment.