Project Case Study
Professional Industrial Pump Manufacturer & Pump Solution Provider
-
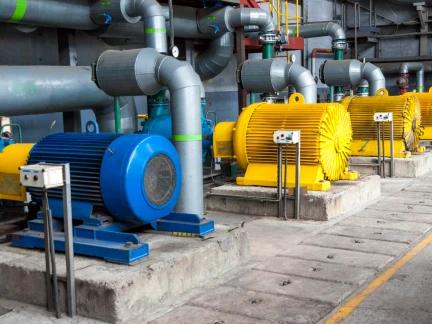
Anhui Mining Slurry Transfer Project
Wear-resistant slurry pumps transferred high-solids tailings over a long pipeline. Liners and impellers were selected for local ore abrasiveness.Learn More -
Sinopec Tanker Unloading System
Twin-rotor pumps completed priming, unloading and tank scavenging for road tankers, including gas-liquid mixed transfer and dry-run stages.Learn More -
Industrial Wastewater Treatment Plant
Closed sewage lifting units collected oily and sludge-laden wastewater and fed the treatment line without odor leakage.Learn More -
Pharmaceutical CIP Transfer System
Sanitary rotary lobe pumps handled CIP fluids and viscous intermediates with polished stainless-steel wetted parts.Learn More -
Agricultural Irrigation Pump Station
Energy-saving pump units with diesel backup served large farmland irrigation during peak season and grid outages.Learn More -
Oil & Fat Processing Rotor Pump Line
High-viscosity rotor pumps transferred crude oil, grease and by-products between tanks with low shear and stable flow.Learn More -
Coal Mine Drainage Pump Unit
Skid-mounted diesel and electric pump sets provided emergency and routine mine drainage with fast on-site commissioning.Learn More -
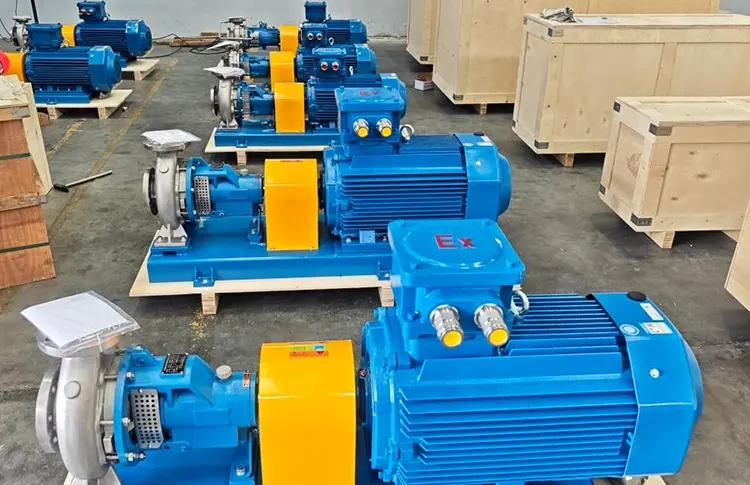
Brine Pretreatment Transfer Project for a Salt Production Plant
Operating Conditions:The pumped medium is saturated brine with a high chloride-ion concentration, containing fine sand and salt particles. The pump is used to transfer brine from the pretreatment…Learn More -
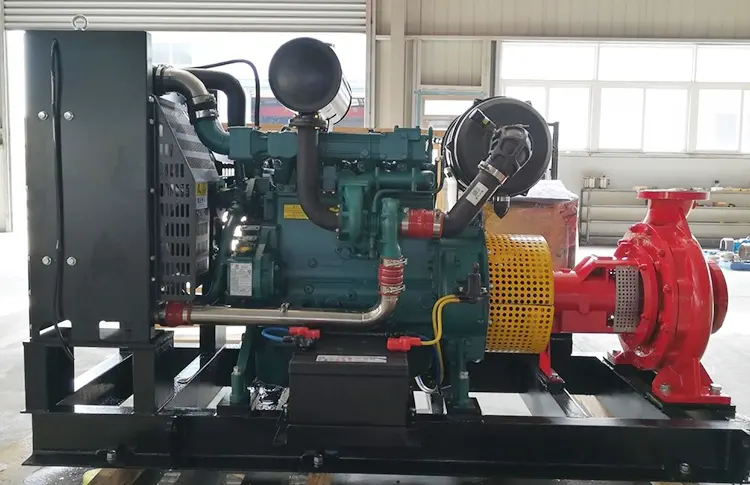
Industrial Park Firefighting Water Supply Project
Operating Conditions:The pumped medium is clean firefighting water at ambient temperature. The pump is used for main firefighting water supply and pipeline pressure stabilization in the industrial park's…Learn More