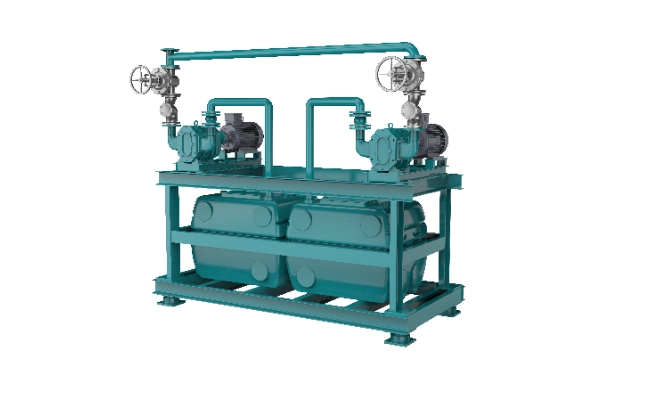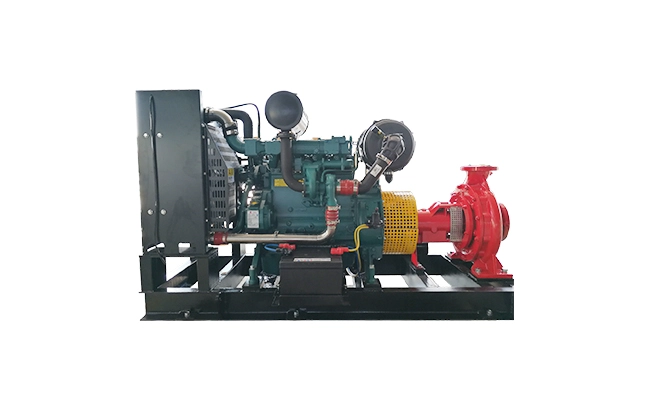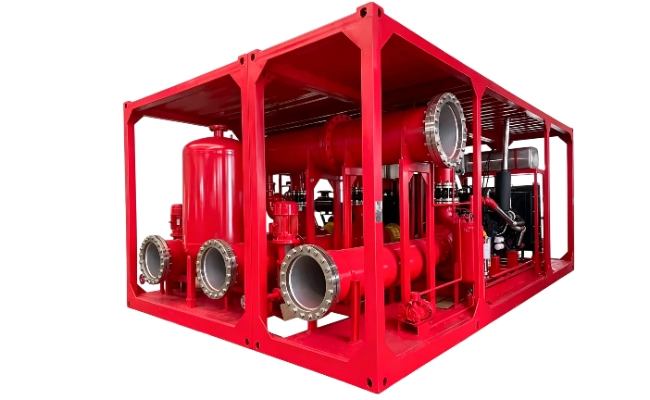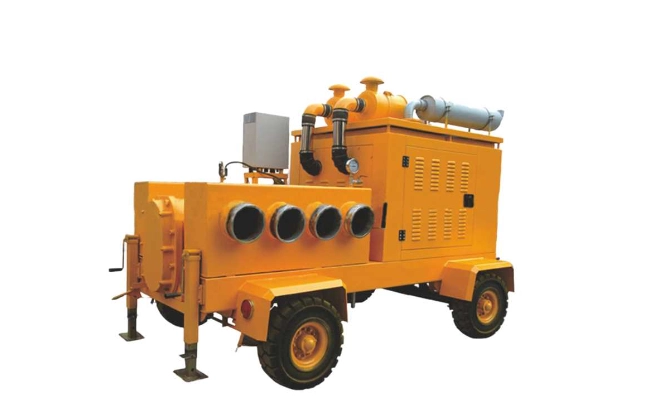
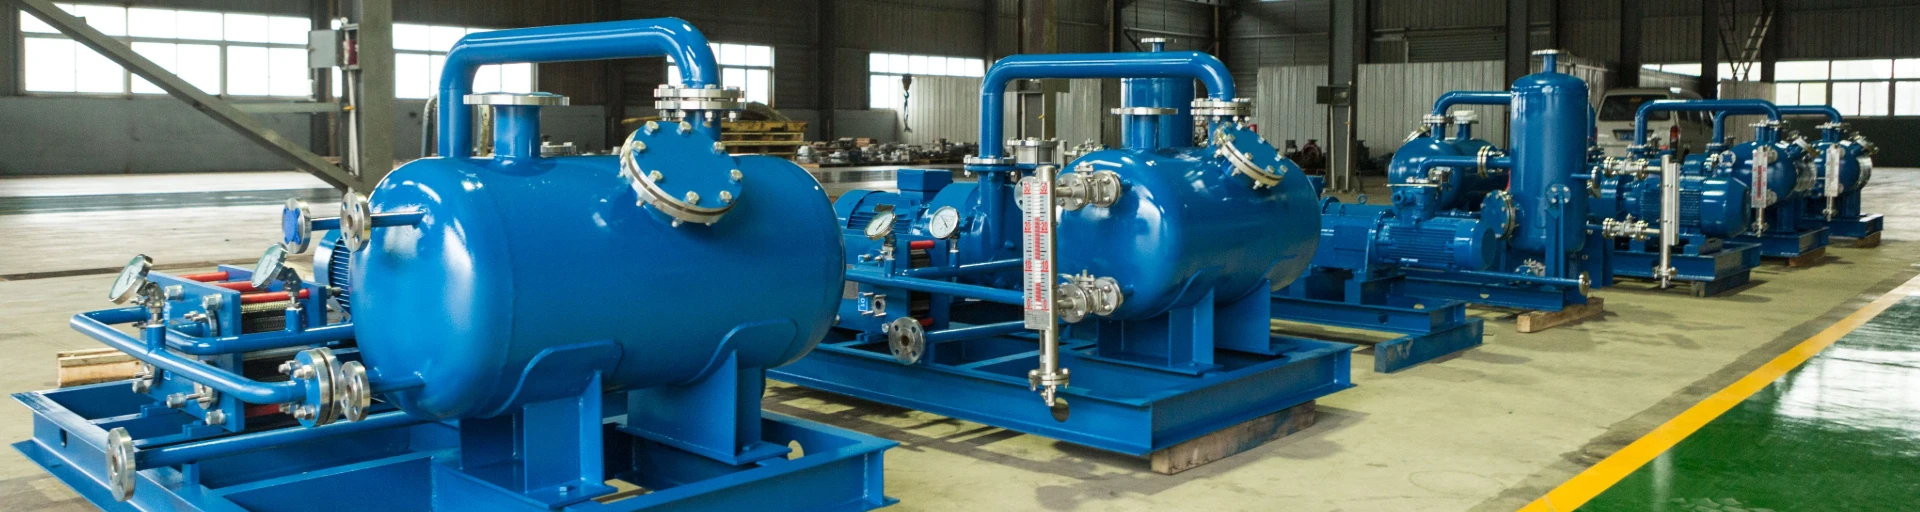
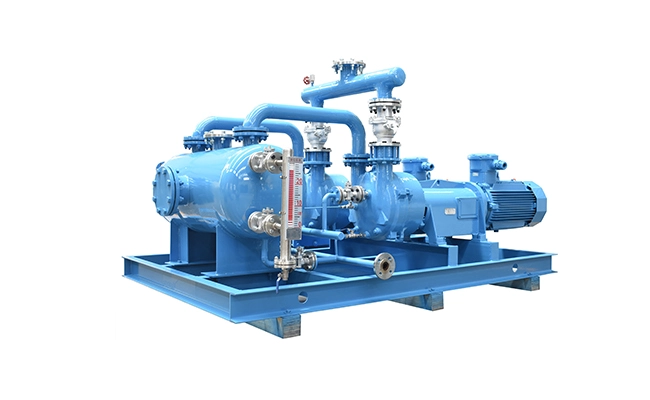
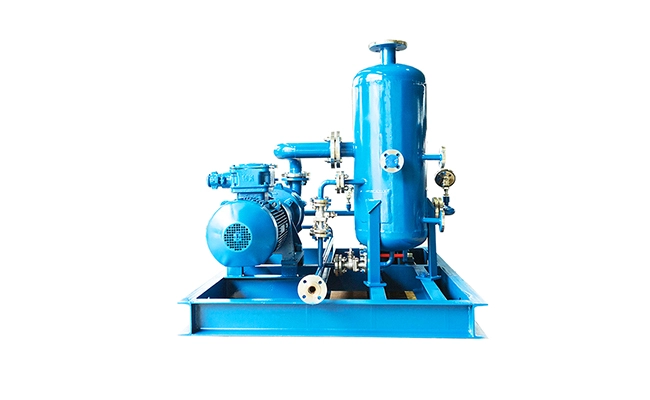
The vacuum pump unit is an integrated packaged vacuum-generating system comprising a main vacuum pump, a backing (foreline) vacuum pump, an electrical control system, a cooling system, a gas-liquid separator, piping and valves, and protective components. Through multi-stage pump trains connected in series for pressure boosting, it rapidly evacuates air, water vapor, condensable gases and trace dust from enclosed spaces and stably establishes and maintains high, medium and low vacuum environments. The complete unit is of skid-mounted, integrated construction with a compact layout, a high degree of automation and stable operation. It can run continuously 24 hours a day at industrial duty and is widely suited to vacuum (negative-pressure) process applications in chemicals, pharmaceuticals, lithium battery, plastics, heat treatment, packaging and environmental waste-gas treatment — it is a core supporting item of modern industrial vacuum processes.
- Description
Core Structure and Working Principle:
The unit uses a multi-stage combination design of a main pump plus a backing pump, working together with an intelligent control system, to solve the problems of insufficient vacuum, slow pumping speed and inability to discharge directly to atmosphere associated with single pumps.
1、Backing (foreline) pump:Responsible for initially evacuating atmospheric gas from the chamber, rapidly reducing the base pressure of the system and creating a low-pressure working environment for the main pump, ensuring efficient start-up and stable operation of the main pump and preventing overload damage.
2、Main pump:Continuously boosts pressure and pumps under low-pressure conditions, greatly increasing the overall pumping speed and ultimate vacuum of the unit and achieving high-precision negative-pressure stabilization.
3、Auxiliary systems:Integrate gas-liquid separation, cooling and buffering, filtration and dust removal, non-return protection and overload alarm devices to effectively separate process water vapor and waste-liquid impurities, prevent gas backflow, pump overheating and ingress of impurities into the pump, and improve equipment durability and process stability.
4、Electrical control system:Equipped with fully automatic start-stop, pressure stabilization and fault self-diagnosis modules; it can automatically regulate pressure by variable frequency according to the set vacuum value, requires no manual attendance and is suitable for use with automated production lines.
Depending on the operating conditions, pump types such as Roots, rotary vane, liquid ring, screw and oil-free dry pumps can be flexibly combined, giving rise to models including corrosion-resistant, oil-free clean, high-pumping-speed industrial and high-temperature corrosion-resistant versions.
-
Q
How do I select the right pump model?
APlease provide medium, viscosity, temperature, required flow, discharge pressure, suction condition and installation space. Our engineers will recommend a rotary pump, centrifugal pump, sewage lifting unit or complete pump set within 24 hours. -
Q
Can the pump handle high-viscosity or solids-laden fluids?
AYes. Twin-rotor lobe pumps are designed for high-viscosity, gas-liquid mixed and slightly solids-laden media. For abrasive slurry, we recommend a dedicated slurry centrifugal pump with wear-resistant materials. -
Q
Do you support OEM / ODM and custom materials?
AWe provide OEM and ODM services, including customized rotor geometry, sealing systems, skid layout, control panels, and wetted parts in cast iron, stainless steel, duplex steel or other alloys. -
Q
What is the warranty and after-sales response?
AStandard warranty is 12 months after handover following 168 hours of trial operation. Technical staff can be dispatched for installation guidance, and quality issues are handled within 0–36 hours after notification.