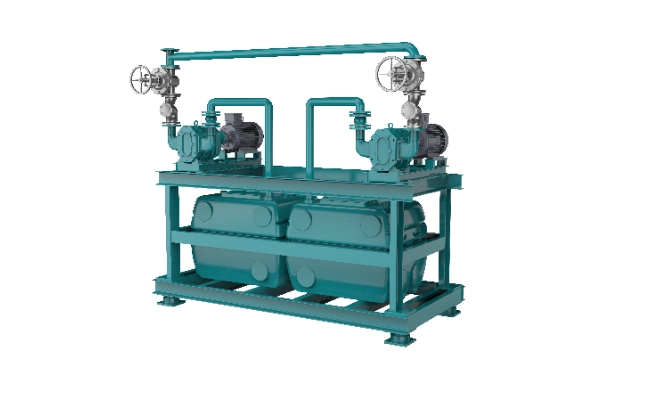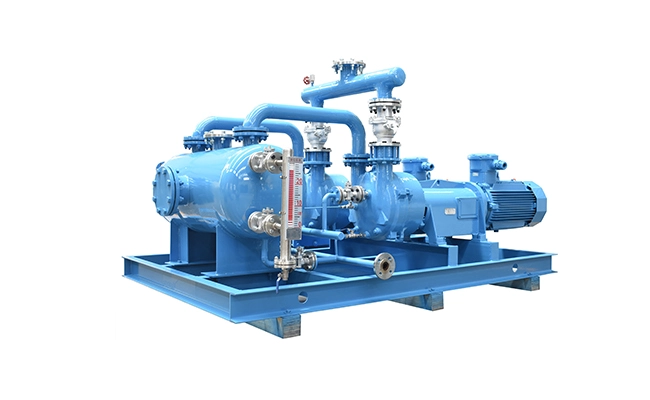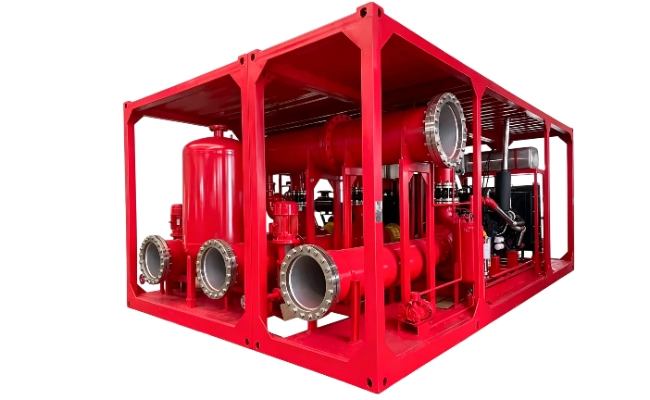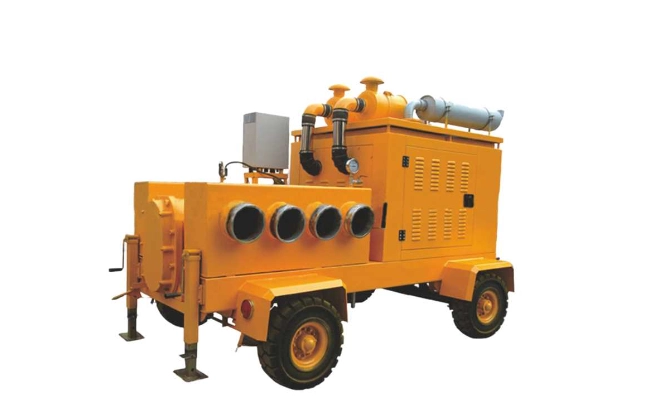
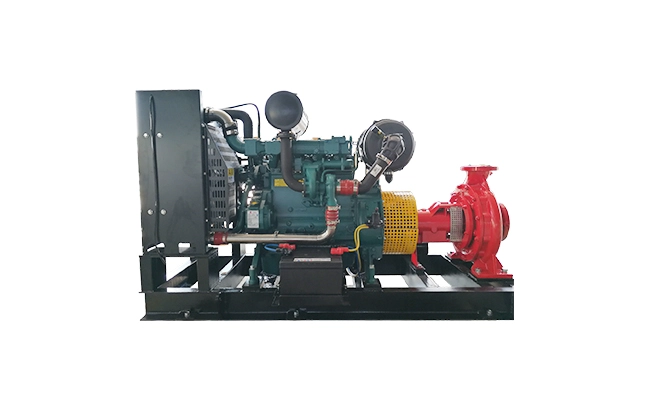
The diesel engine pump unit is a self-contained emergency fluid-transfer package for use where no power supply is available. Using a diesel engine as an independent power source and requiring no external electricity, it integrates a diesel engine, a centrifugal pump / self-priming pump or rotary lobe pump, an intelligent control system, a fuel system, a cooling system, baseframe piping and safety protection devices into a single skid-mounted unit. The equipment can operate completely independently of the mains supply, solving problems of water supply, drainage, pressure boosting and emergency firefighting under power failure, power cut or no-power conditions. It features rapid starting, strong power, all-weather standby readiness and extremely high reliability, and is widely used in critical applications such as emergency firefighting, municipal flood drainage, industrial standby water supply, mine emergency response, farmland irrigation, construction site work and emergency make-up water in chemical plants. It is an essential first-tier emergency fluid-handling facility for all types of projects.
- Description
Structure and Working Principle:
The complete unit adopts an integrated transmission structure in which the diesel engine is directly coupled to the pump body through a flexible coupling. This gives high transmission efficiency, few failure points and fast response, with a simple, durable overall structure that is easy to maintain.
Prime mover (diesel engine)
An industrial-grade diesel engine is used, with ample power reserve, high torque and strong load resistance, supporting cold starting at low temperature and continuous full-load operation. It is equipped with an independent fuel tank, a lubricating oil system and air-cooled / water-cooled heat dissipation systems to ensure long continuous operation without overheating or stalling, and is suited to harsh conditions such as remote sites, heavy rain, high temperature and severe cold.
Pump body
Depending on the operating conditions, pump types such as single-stage centrifugal pumps, multistage booster pumps, high-capacity double-suction pumps, rotary lobe pumps and self-priming sewage pumps can be selected. The optimized hydraulic design provides high efficiency, low NPSH required and smooth passage of the pumped medium. The pump handles clean water and water with light impurities, delivering high capacity, high head and good pressure stability to meet different process requirements such as low-pressure high-volume and high-pressure long-distance transfer.
Intelligent control system
Equipped with a fully automatic intelligent control module, it provides automatic start on mains failure, manual start, remote start and pressure-linked start functions. It continuously monitors speed, water temperature, oil pressure, discharge pressure and running hours, and incorporates fault alarm, shutdown protection, automatic preheating and automatic pressure stabilization functions, enabling unattended emergency interlock operation.
Auxiliary systems
Integrates a vibration-damping baseframe, suction and discharge piping, valve assemblies, a complete fuel supply package, an exhaust silencer and a weatherproof enclosure. The complete unit is skid-mounted and integrated, ready for use once positioned, with no complex civil works required.
-
Q
How do I select the right pump model?
APlease provide medium, viscosity, temperature, required flow, discharge pressure, suction condition and installation space. Our engineers will recommend a rotary pump, centrifugal pump, sewage lifting unit or complete pump set within 24 hours. -
Q
Can the pump handle high-viscosity or solids-laden fluids?
AYes. Twin-rotor lobe pumps are designed for high-viscosity, gas-liquid mixed and slightly solids-laden media. For abrasive slurry, we recommend a dedicated slurry centrifugal pump with wear-resistant materials. -
Q
Do you support OEM / ODM and custom materials?
AWe provide OEM and ODM services, including customized rotor geometry, sealing systems, skid layout, control panels, and wetted parts in cast iron, stainless steel, duplex steel or other alloys. -
Q
What is the warranty and after-sales response?
AStandard warranty is 12 months after handover following 168 hours of trial operation. Technical staff can be dispatched for installation guidance, and quality issues are handled within 0–36 hours after notification.